Kerogen Systems Inc.
Engineering a domestic, lower-carbon source of industrial carbon
KSI is an engineering, research, and development company commercializing patented technology that converts kerogen into Kerogenate — a domestic carbon feedstock that displaces crude-derived petrochemicals and lowers the carbon intensity of the products made from them.
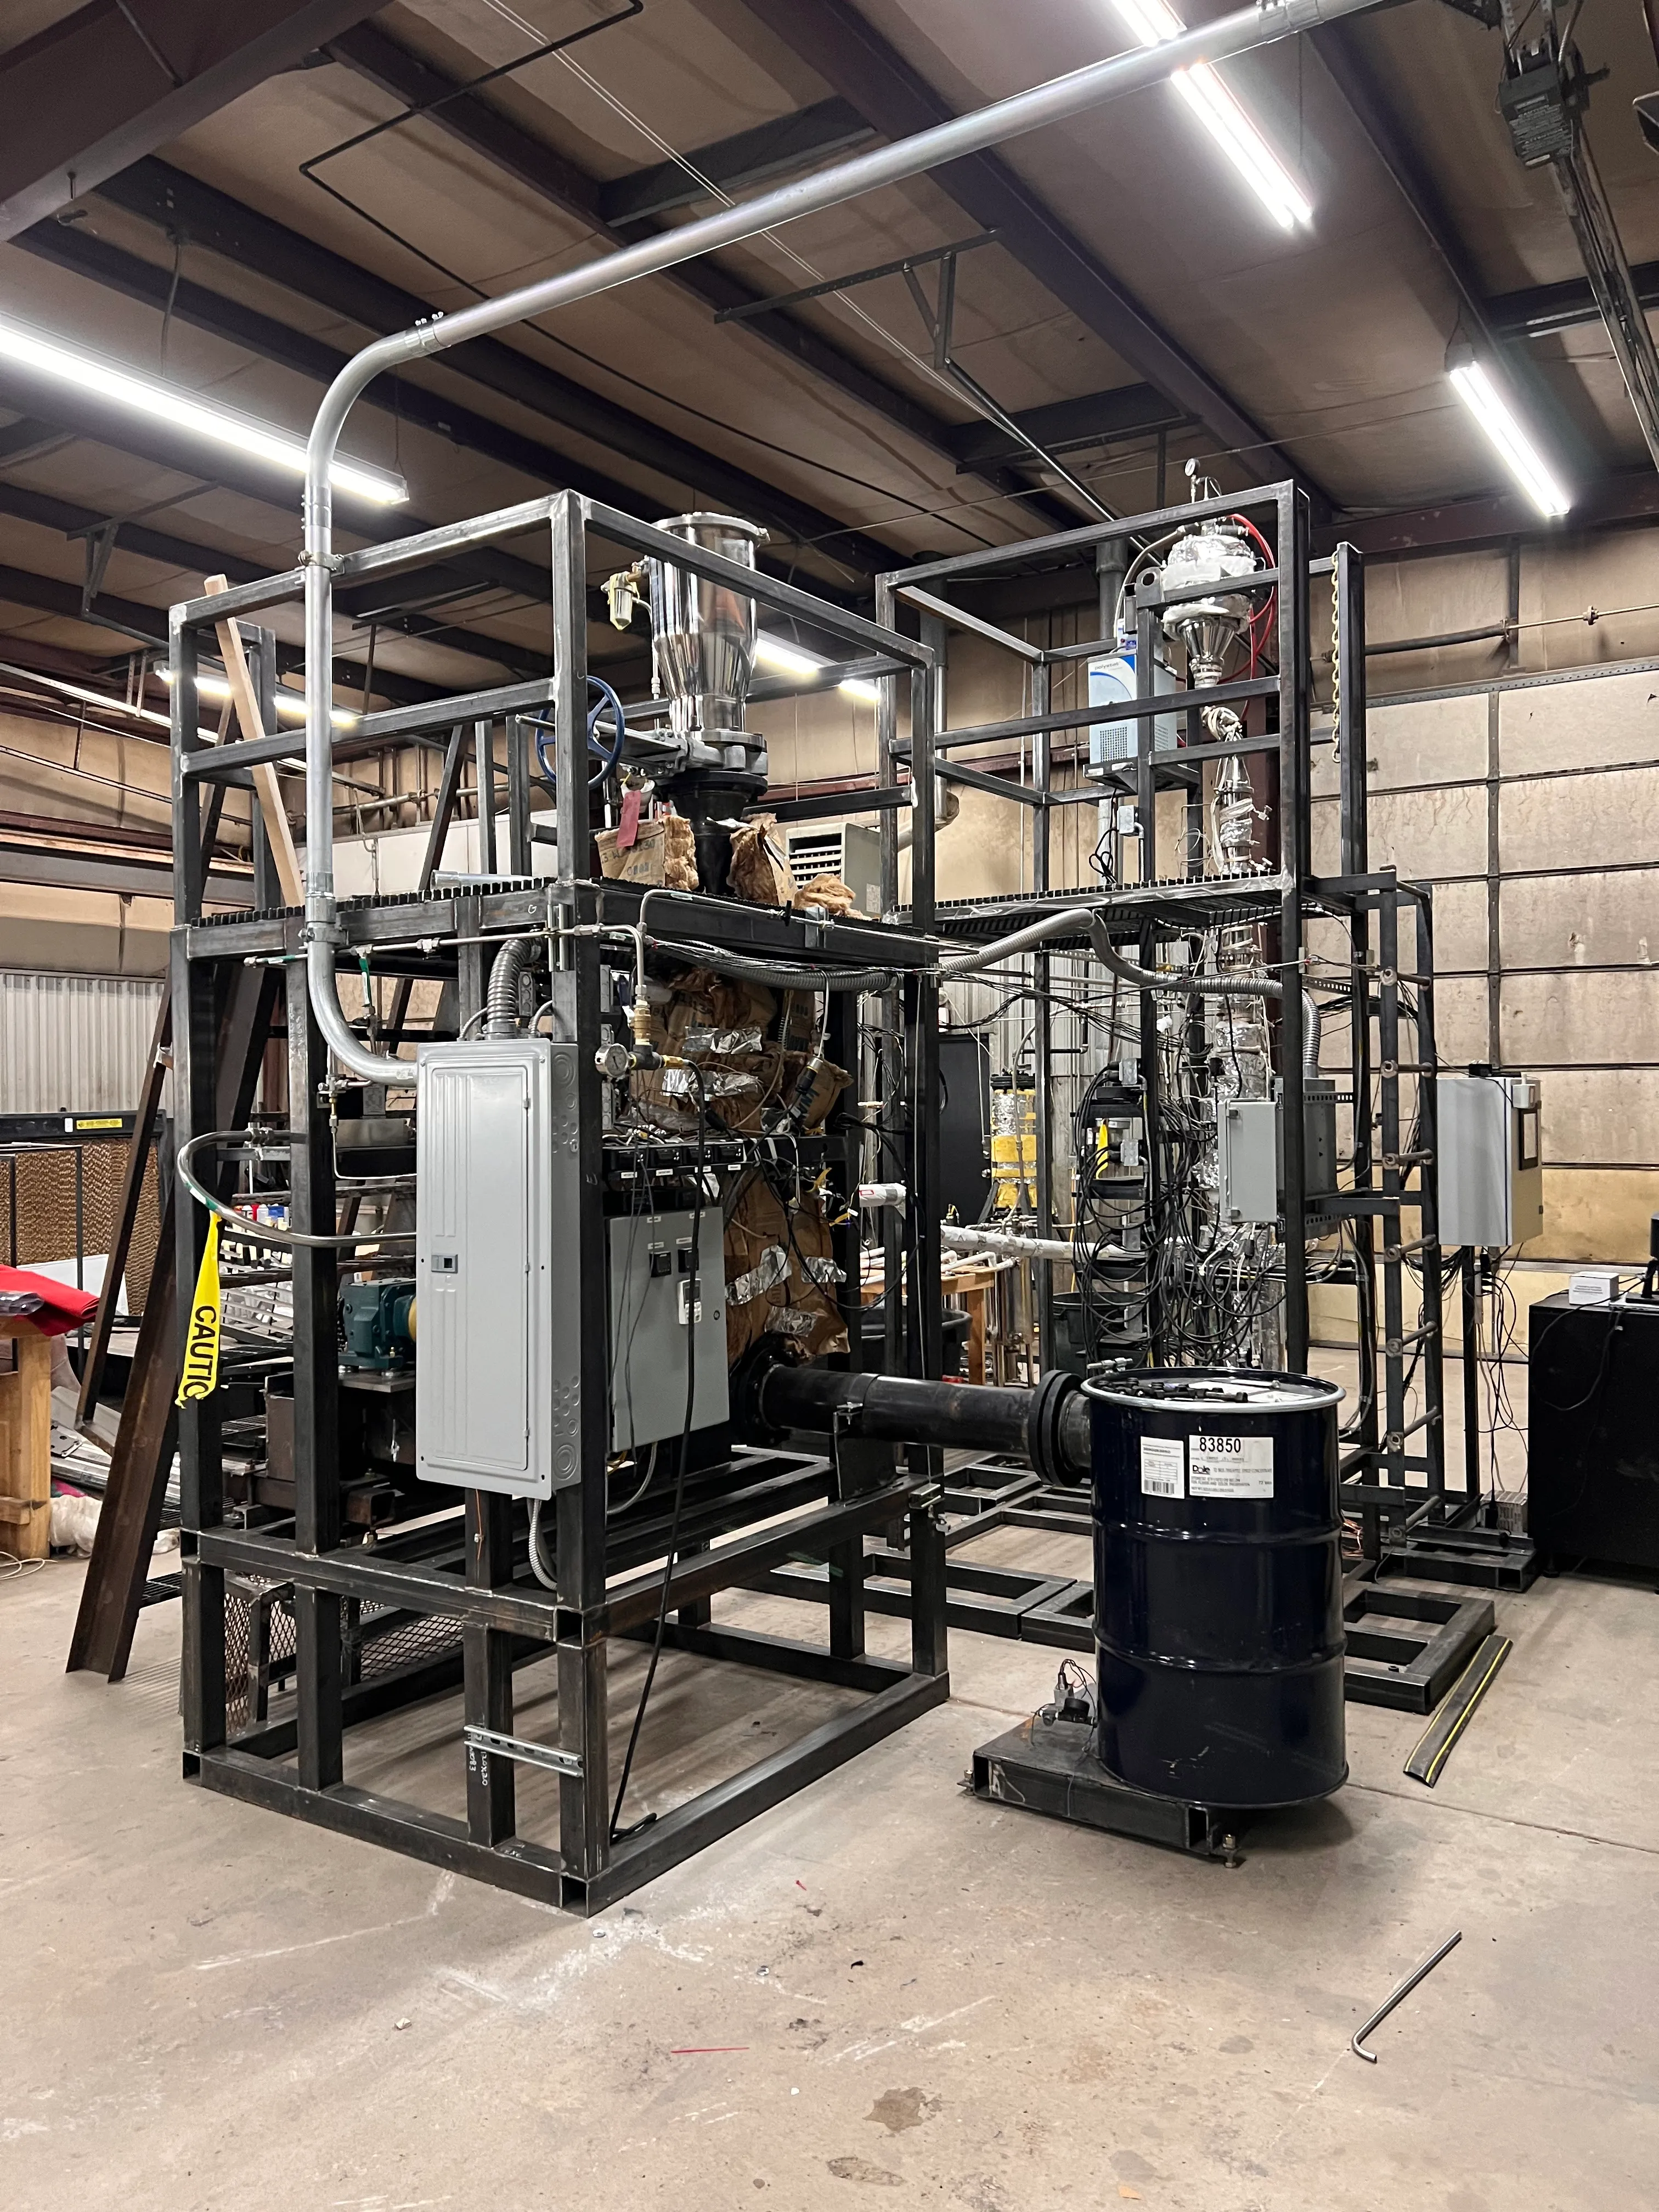
Demonstrated at pilot scale in Vernal, Utah, and protected by two granted U.S. patents.
See it for yourself: request a Kerogenate sample kit and evaluate the feedstock in your own lab.
Leadership
Decades of industrial and process experience
Experimental research, refining technology commercialization, pilot plant design and scale-up, process engineering, financial strategy, and information systems — the full span of skills needed to take a novel process from the bench to a commercial plant.
Otto Schneider
Founder & Chief Executive Officer
Paul Owen
President of Technology
Taylor Lewis
President & Chief Capital Officer
Sabra Ehrhart
President & Chief Operating Officer
Patented Technologies
A novel retort that turns kerogen into low carbon-intensity products
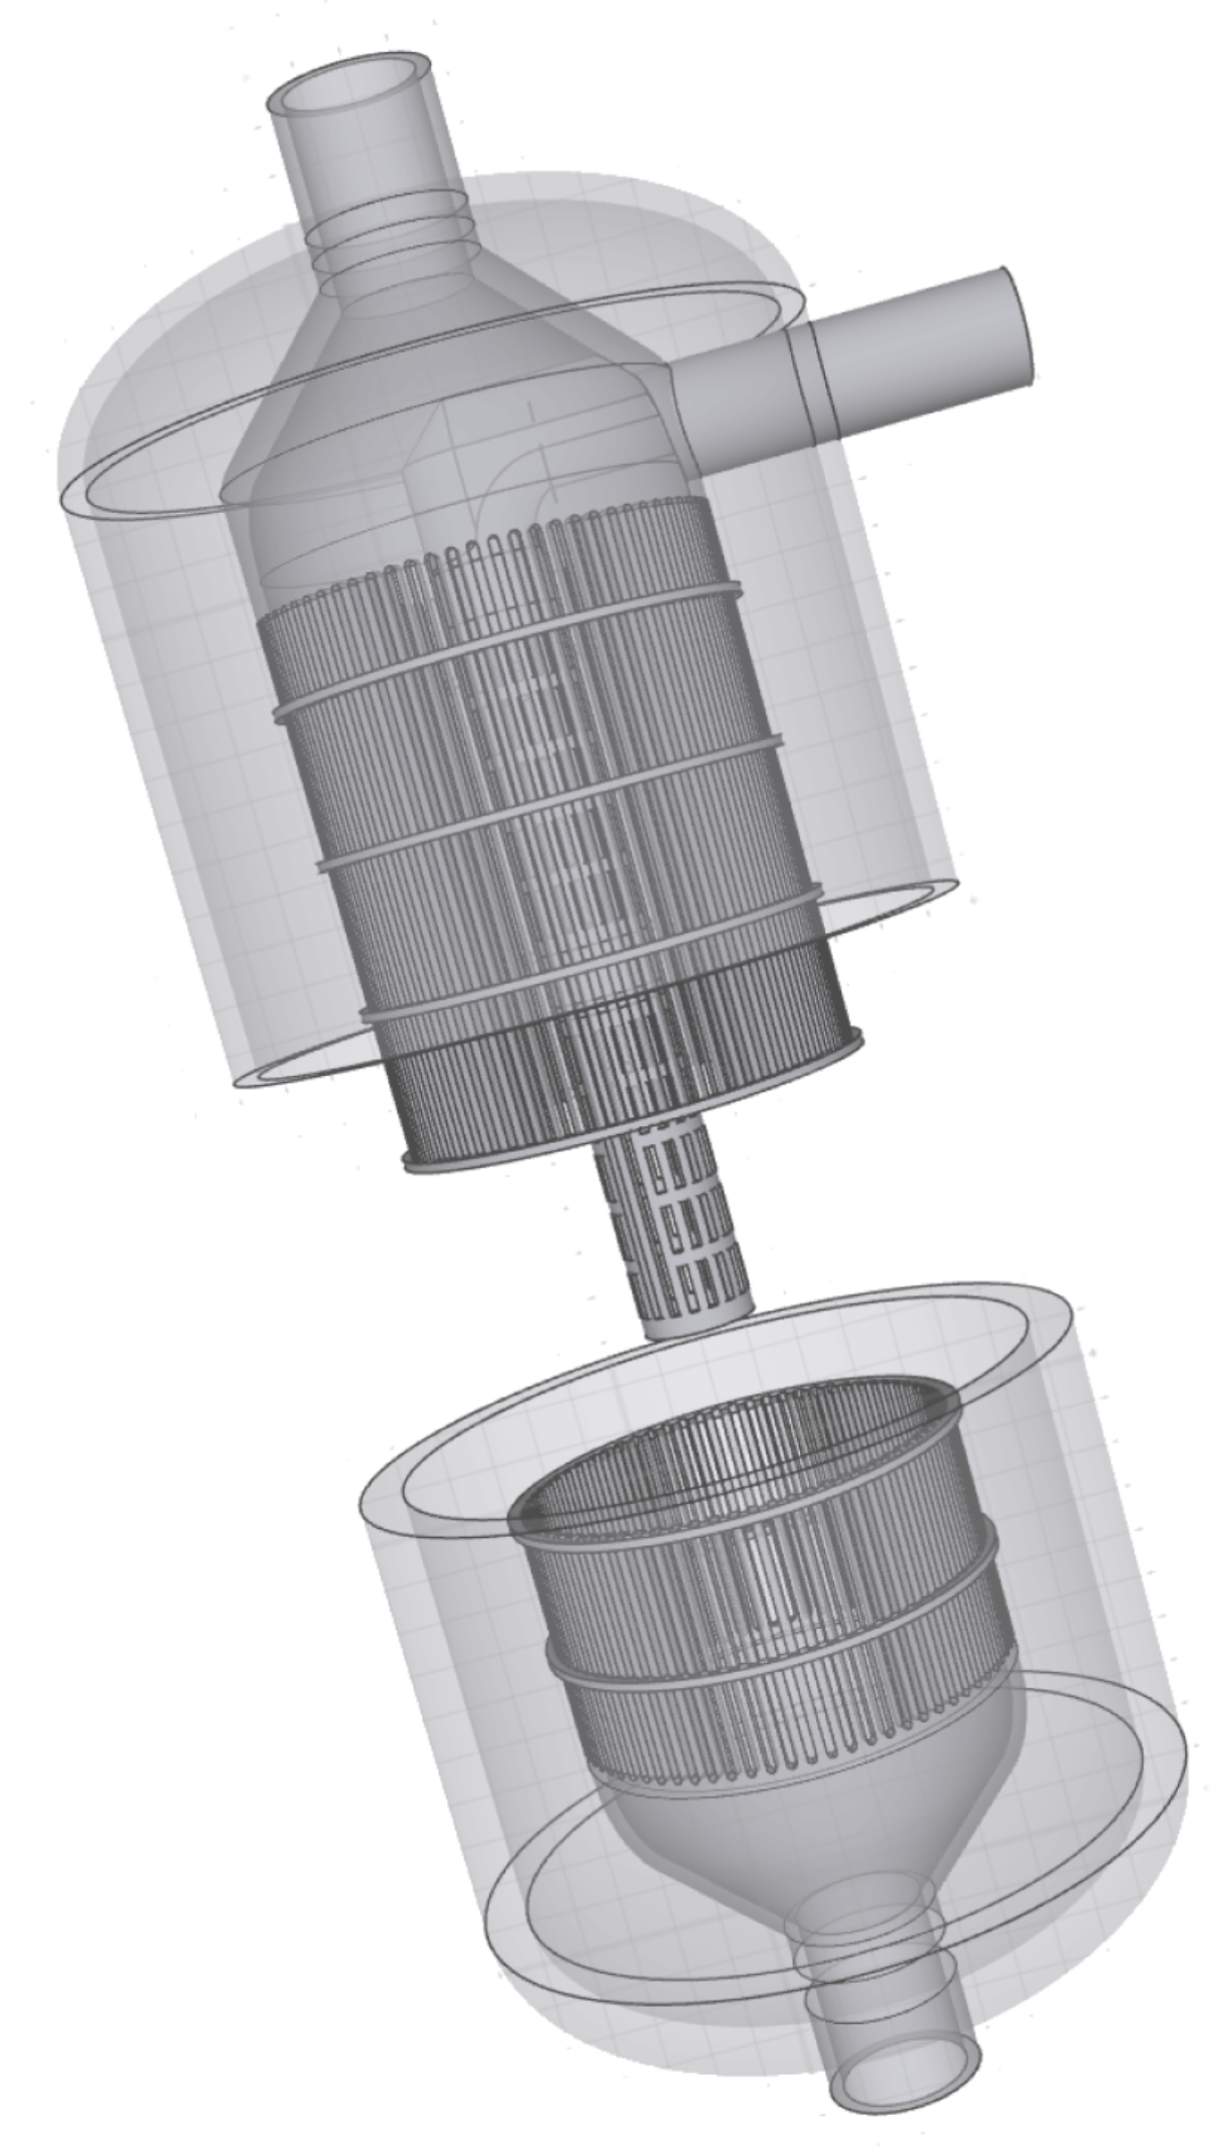
Kerogen is a large, solid, organic macro-molecule found in certain sedimentary rocks — the raw material from which crude oil and natural gas form, given enough geological heat and time. Rather than waiting on geology, our patented process applies controlled pyrolysis to transform kerogen directly into a versatile oil we call Kerogenate: a rich mixture of carbon compounds from light gases through mid-distillates to heavy asphaltenes, resins, and pitch. A single cubic yard of ore from the Mahogany Zone of the Green River Formation yields approximately one barrel — a minimum of 23 U.S. gallons per ton.
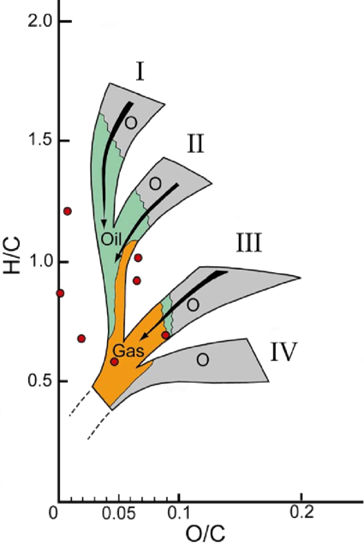
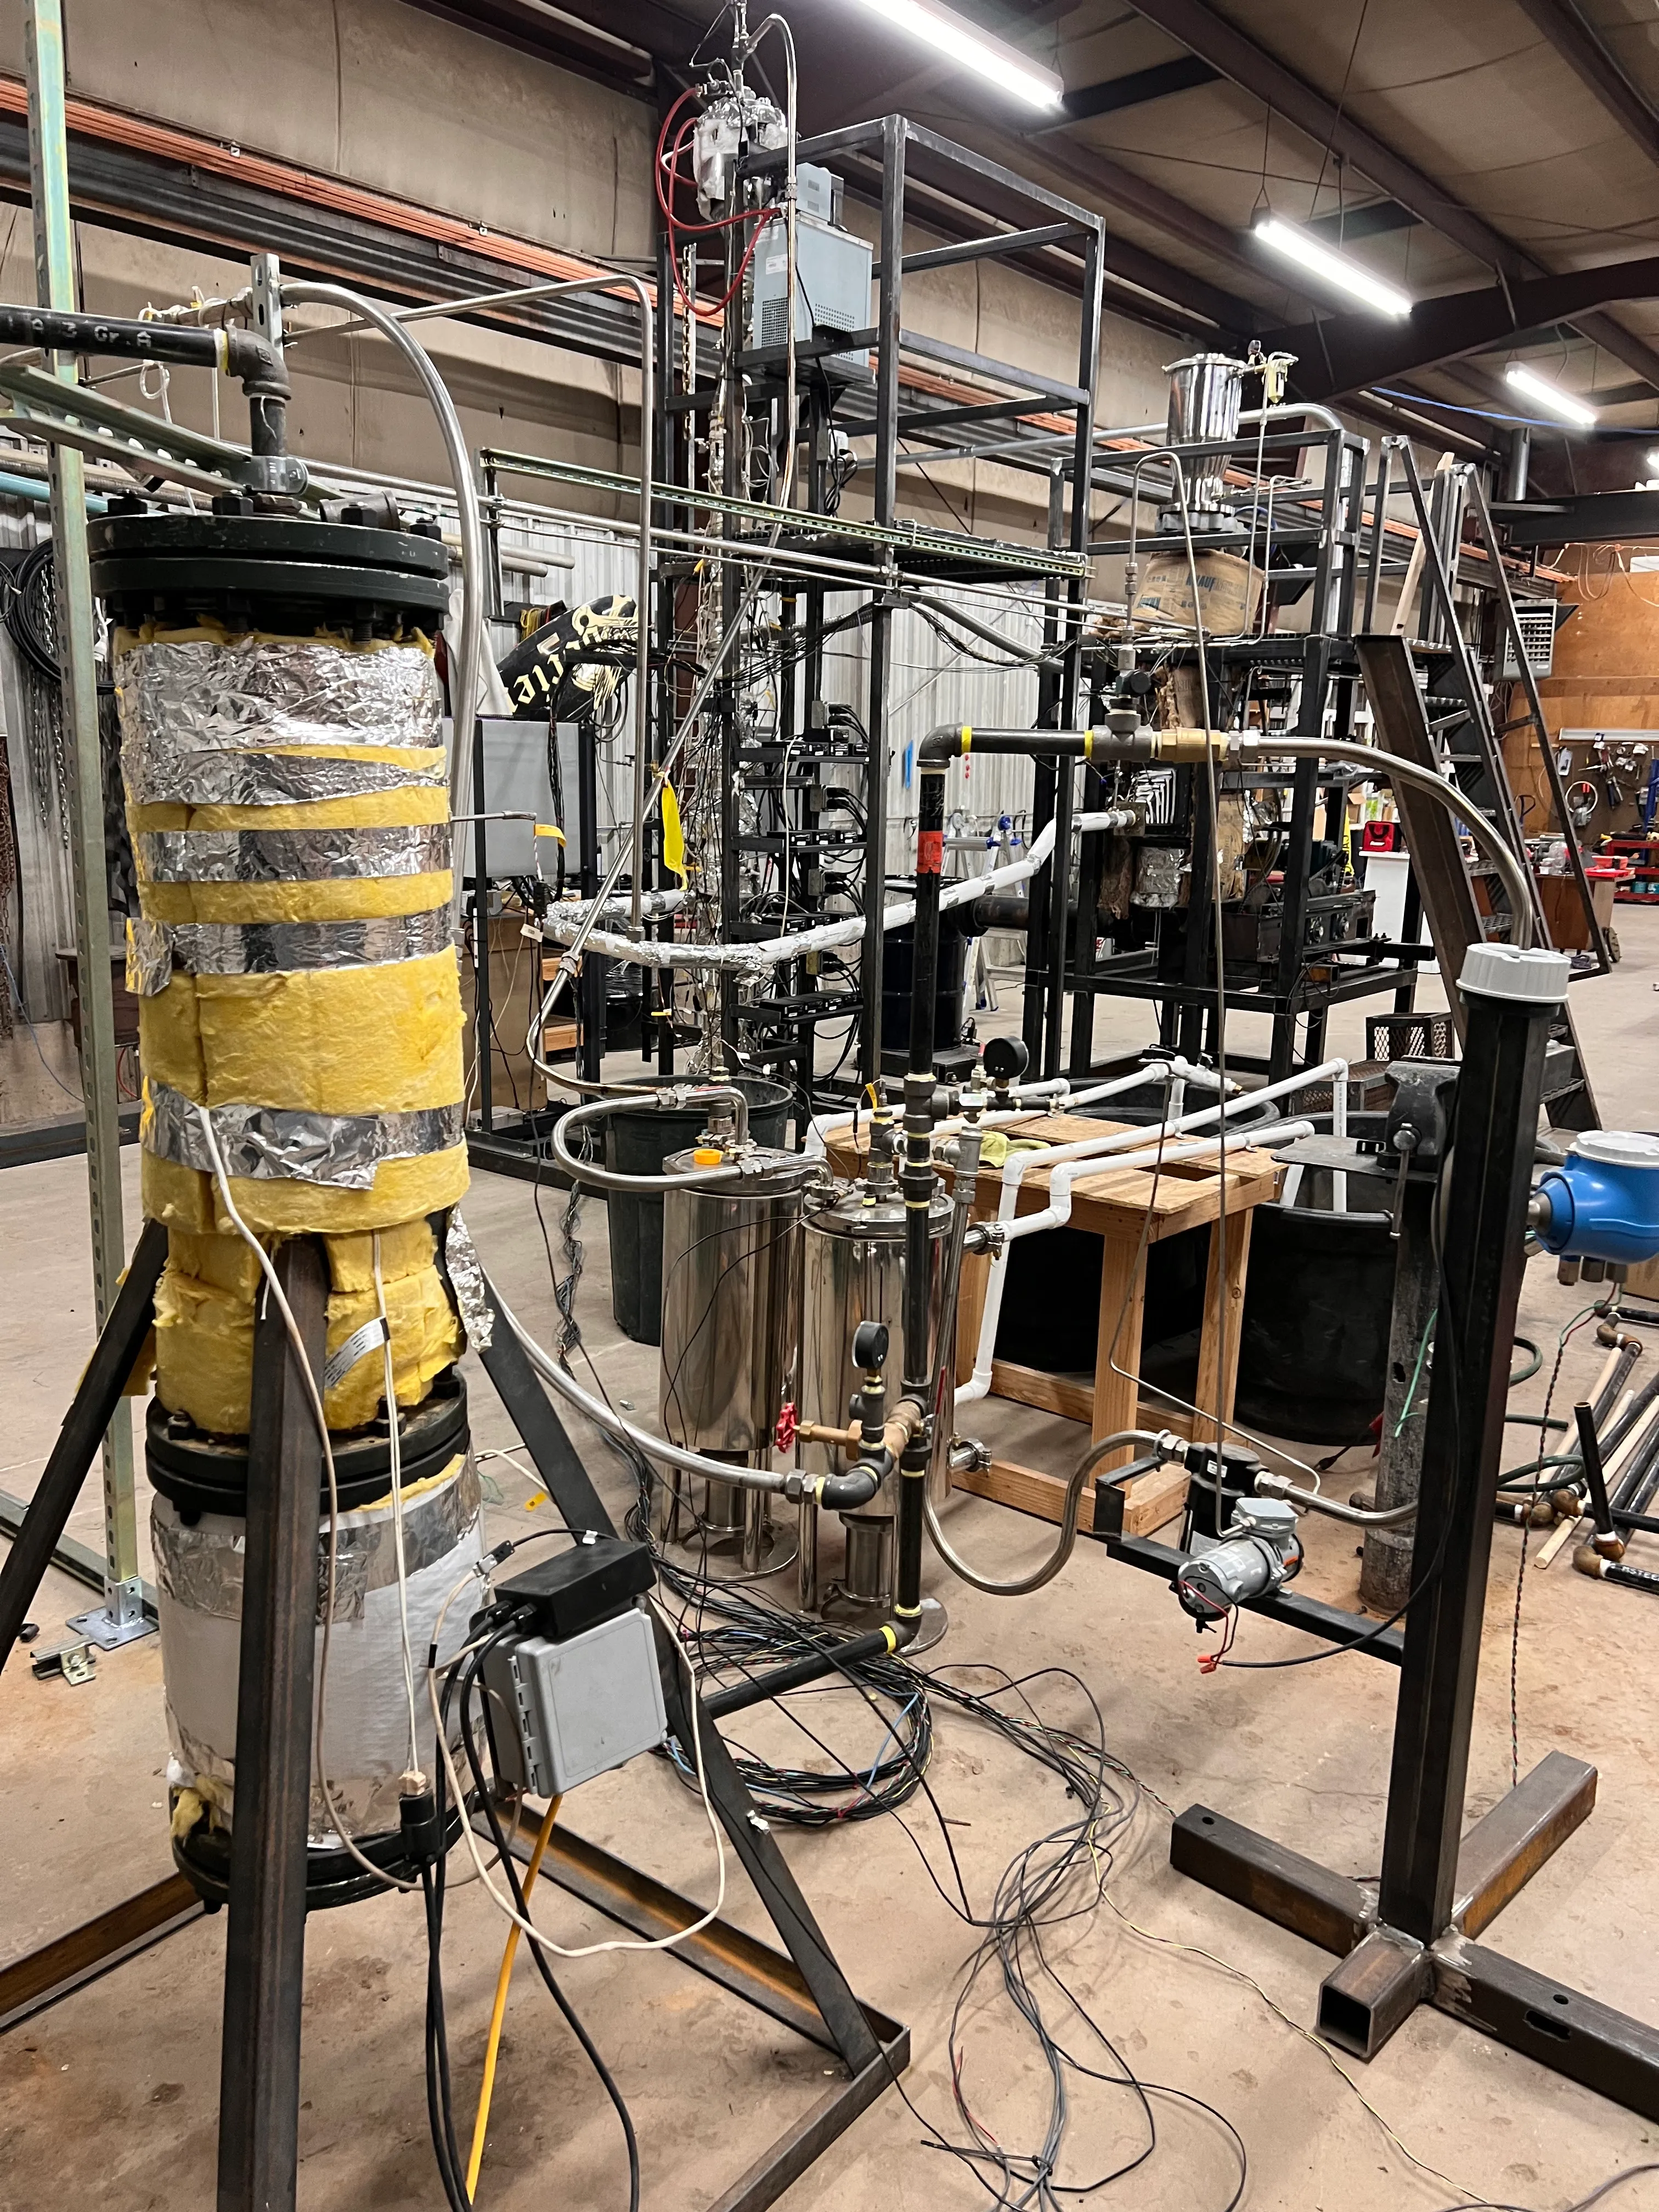
At the core of our process is the Thin Bed Cross-flow Retort (TBCR), coupled to a fractionation column. Together they perform what we term KTC — Kerogen To Chemicals — transforming kerogen ore into Kerogenate and separating it into product fractions in a single integrated operation, protected by two granted U.S. patents (US20180355254A1 and US20210054290A1).
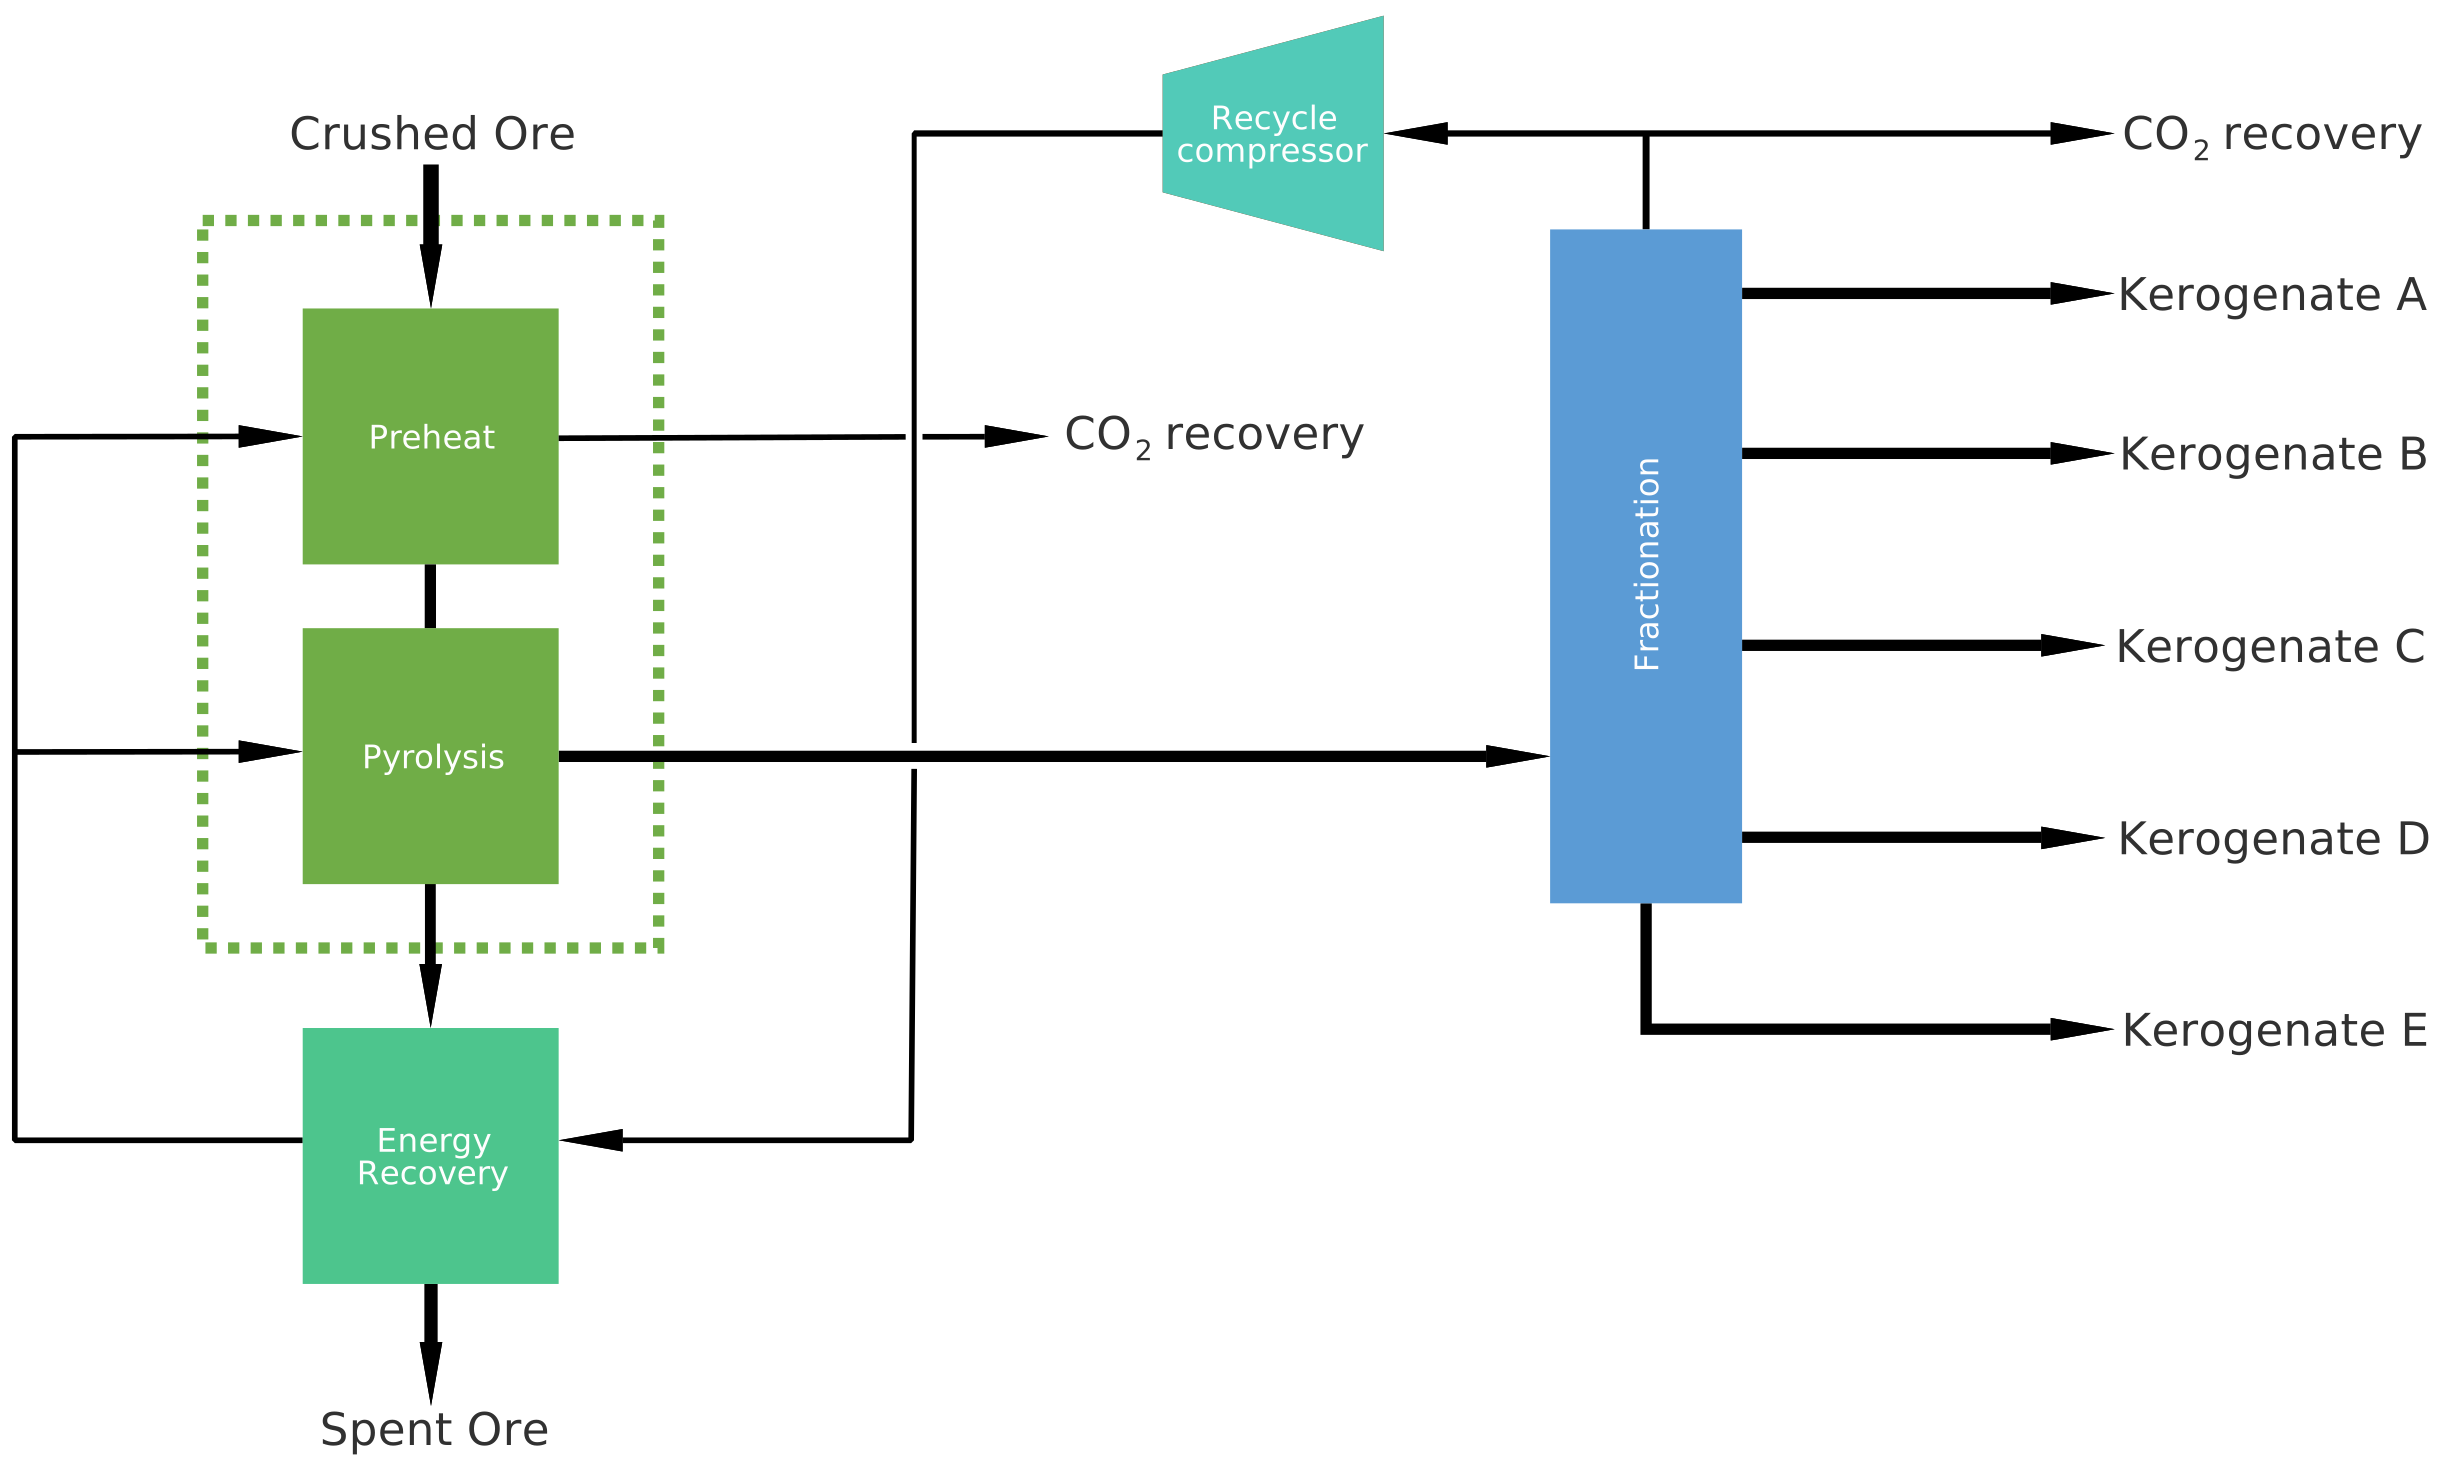
Sustainability is designed in, not added on. Where legacy retorting combusts fossil fuels for heat, the TBCR uses renewable electrical and radio-frequency heating — the key to Kerogenate's low carbon intensity. KTC also manages heteroatoms such as nitrogen, sulfur, and arsenic, raising product value across agrochemicals, pharmaceuticals, surfactants, solvents, polymers, asphalt, and carbon-carbon composites.
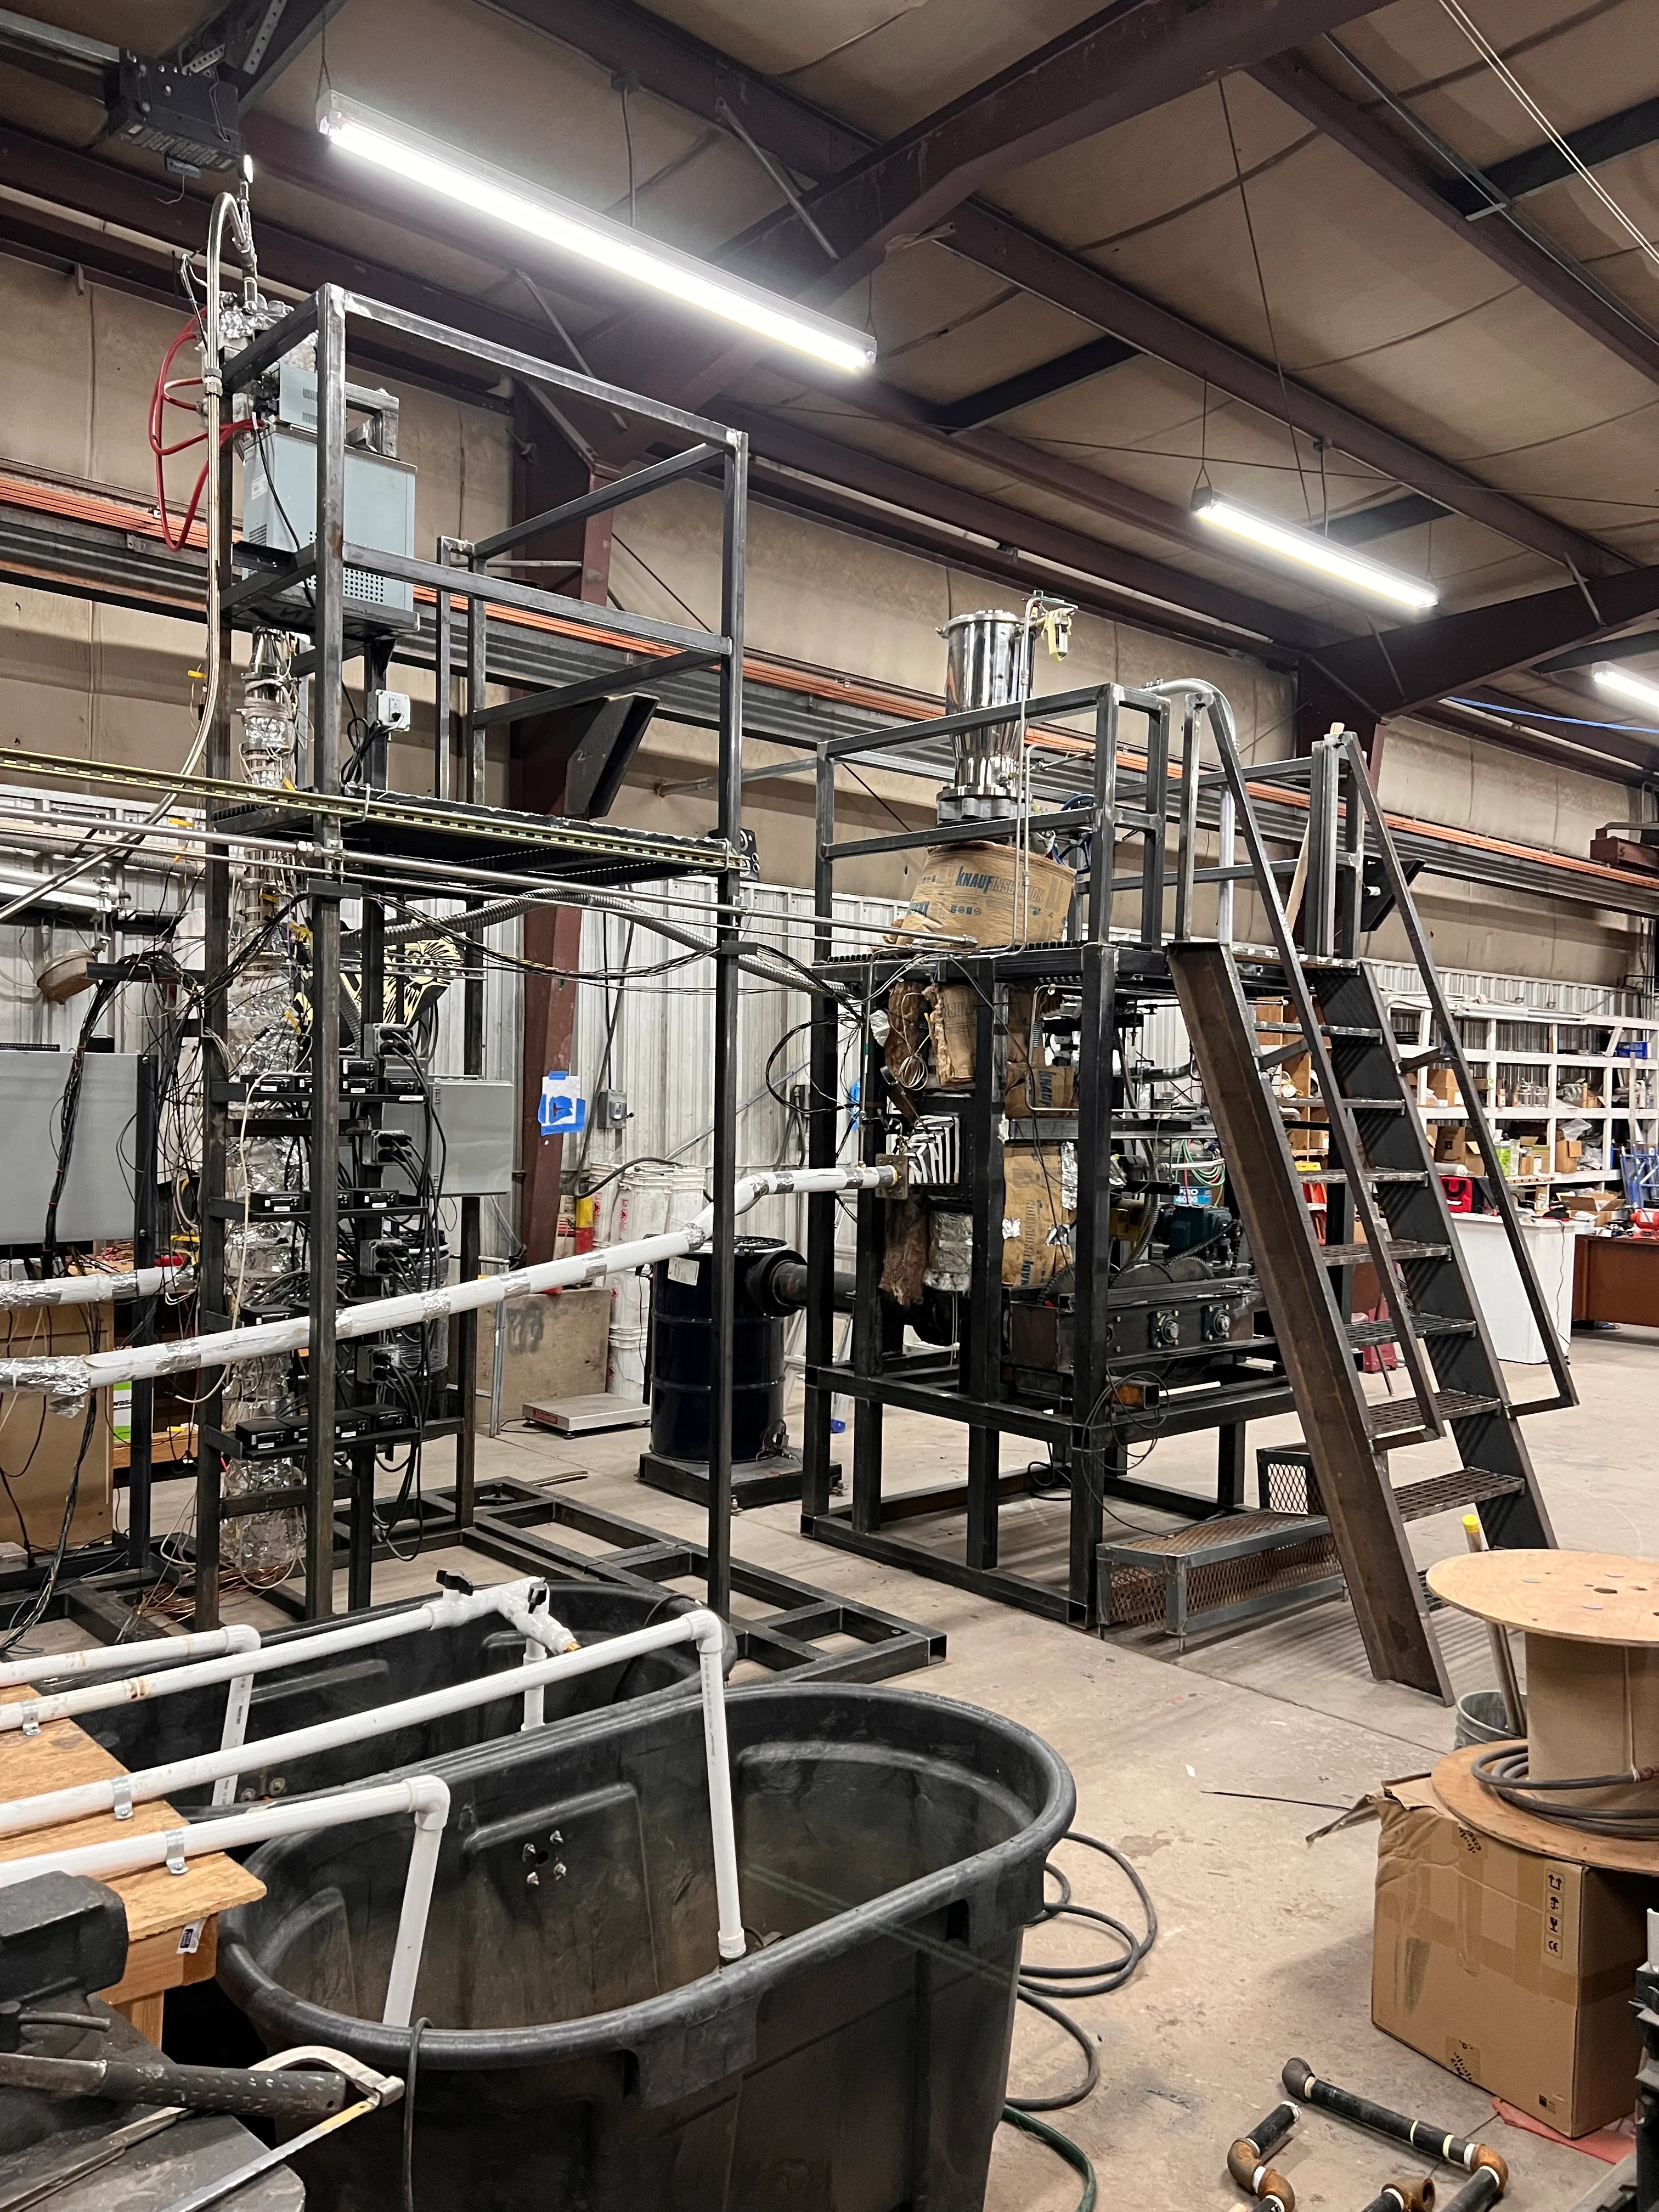
The technology is proven, not theoretical: the Vernal pilot plant — built with private funding and a USTAR-TAP grant — has demonstrated the commercial potential of kerogen retorting for carbon products, and a full life cycle assessment (LCA) of the process has been completed. Commercialization follows three phases: Phase 1 operates the pilot plant in batch mode to establish the product slate and develop markets; Phase 2 uses pilot data for modelling and scale-up to design the first commercial plant; Phase 3 builds and operates it.
Proven at pilot scale in Vernal, Utah
A decade of development: research into kerogen processing began in 2015, the retort design was proven and the first patent granted in 2018, the pilot plant fulfilled its USTAR objectives in 2019, Kerogen Systems Inc. was founded in 2020, and the second patent was granted in 2021. Along the way we work with Idaho National Laboratory on Field Assisted Sintering Technology (FAST) for continuous carbon-carbon composite manufacture; the Miller Advanced Research and Solutions (MARS) Center at Weber State University on carbon-carbon, carbon-silicon, and other advanced materials; and Hexcel, one of the nation's leading manufacturers of carbon fiber and carbon-carbon composites for aerospace.
Beyond the first commercial unit, our CEPAC (Carbon Extraction, Processing And Conversion) manufacturing hub concept is an integrated chemical production complex, vertically integrated from resource to finished product. Resource and technology ownership shorten time to revenue; the model is aligned with state and local development goals and suited to private equity, venture capital, and government programs. Our business model is build and operate, with licensing to follow.